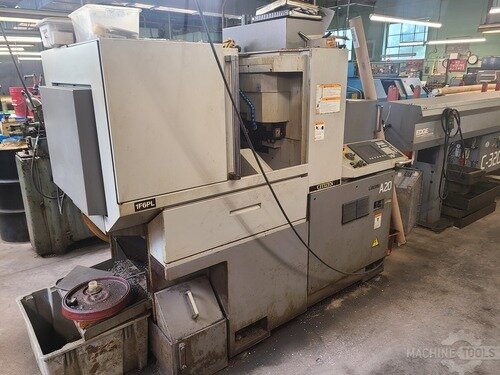
USED CITIZEN A20VI – 2009
The 2009 CITIZEN A20VI is a precision CNC Swiss-type sliding headstock lathe designed for high-volume production of small-diameter, high-precision components. Manufactured by Citizen Machinery, the A20VI is built around a compact 20 mm machining capacity and combines sliding-headstock turning, C-axis machining, live tooling, and a sub-spindle within a single production platform. This configuration allows manufacturers to perform turning, drilling, tapping, milling, and rear-end machining operations with minimal workpiece handling. The machine is particularly suited for manufacturers producing small precision components in large quantities where repeatability, cycle-time efficiency, and automated production are important.
The A20VI provides a maximum machining diameter of approximately 20 mm and a maximum machining length of approximately 165 mm per chucking on documented 2009 configurations. Its compact machining envelope is specifically optimized for small-diameter components rather than large conventional turning applications. The sliding-headstock design supports the workpiece close to the cutting tools, helping provide stability when machining long, slender components that could otherwise be difficult to support using a conventional fixed-headstock lathe. (cncbul.com)
One of the machine’s primary advantages is its ability to combine multiple machining processes within a compact Swiss-type platform. The A20VI can perform conventional turning operations along with front-end drilling, live-tool cross machining, tapping, and rear-end operations using its sub-spindle. This reduces the need to transfer small components between separate machines and can improve dimensional consistency between multiple features.
The main spindle on documented A20VI configurations operates at up to approximately 8,000 RPM, while the back spindle can also reach approximately 8,000 RPM. Some A20-family specifications identify configurations capable of up to 10,000 RPM, so the exact spindle rating should be verified against the individual 2009 machine and its original specification. The high spindle speed is particularly useful for machining small-diameter components where higher rotational speeds can support efficient cutting and improved surface finishes. (machinetools.com)
The A20VI uses full C-axis indexing on both the main and back spindles, with documented specifications identifying approximately 0.001-degree indexing capability. This allows precise spindle positioning for milling, drilling, cross-hole machining, and other operations requiring controlled angular orientation. (machinetools.com)
The machine’s live tooling system further expands its machining flexibility. Documented A20VI configurations provide multiple live-tool positions on the main slide, with rotary tooling speeds of approximately 6,000 RPM. This allows manufacturers to perform cross milling, drilling, tapping, and related secondary operations without moving the workpiece to another machine. (toolquipusa.com)
The sub-spindle is another important component of the A20VI’s production capability. With a maximum back-spindle chucking diameter of approximately 20 mm and speeds up to approximately 8,000 RPM, the sub-spindle can grip the workpiece for rear-end machining operations. This enables manufacturers to complete front and back features within one automated production cycle.
The machine is capable of machining a wide variety of small-diameter materials including stainless steel, carbon steel, aluminum, brass, bronze, titanium, medical alloys, engineering plastics, and other precision materials. Proper tooling, cutting parameters, coolant delivery, and material-specific machining strategies remain important for achieving optimal results.
The A20VI is particularly well suited for manufacturing components such as miniature shafts, pins, connectors, fittings, bushings, medical components, electronic hardware, precision fasteners, valve components, and small mechanical assemblies. Its Swiss-type architecture is especially valuable when producing long or slender components where close tool support is required.
Many used 2009 A20VI machines are equipped with production accessories such as magazine bar feeders, chip conveyors, parts catchers, coolant systems, mist collectors, high-pressure coolant systems, and automatic fire-suppression equipment. Documented 2009 machines have been offered with Edge Technologies C-320 magazine bar feeders, chip conveyors, parts catchers, high-pressure coolant, and mist collection systems. (machinetools.com)
The machine can also support automated bar-fed production, making it especially useful for high-volume manufacturing environments. A long magazine bar feeder can supply material continuously, allowing the machine to produce large quantities of small components with limited operator intervention.
The A20VI’s compact footprint is another advantage for manufacturers with limited floor space. Despite its relatively small physical size, the machine integrates multiple machining functions, allowing a single production cell to perform operations that might otherwise require several conventional machines.
The CNC control system on documented 2009 machines is commonly FANUC-based, with some machines equipped with Citizen Cincom control configurations depending on market and machine specification. Buyers should verify the exact control installed on the individual machine before purchase. (machinetools.com)
The A20VI is especially attractive for manufacturers producing repetitive small components where cycle time, automation, and dimensional repeatability are important. Its combination of sliding-headstock machining, live tooling, C-axis capability, and sub-spindle functionality provides considerable flexibility within a relatively compact machine platform.
Industries including medical manufacturing, electronics, aerospace, automotive, telecommunications, hydraulic equipment, instrumentation, and precision contract machining can utilize the A20VI for producing small, complex components.
Because of its precision-oriented Swiss-type architecture, automated production capability, live tooling, sub-spindle, and compact 20 mm machining capacity, the 2009 CITIZEN A20VI remains a useful used CNC Swiss lathe for manufacturers requiring efficient small-part production.
CITIZEN A20VI – AXIS
| SpecificationDetails | |
|---|---|
| Machine Configuration | CNC Swiss-Type Sliding Headstock Lathe |
| Axis Configuration | Multi-Axis CNC |
| Main Machining Diameter | Approx. 20 mm |
| Main X1 Rapid Traverse | Approx. 18 m/min |
| Other Axis Rapid Traverse | Approx. 32 m/min |
| Main Spindle C-Axis | Full C-Axis |
| Sub-Spindle C-Axis | Full C-Axis |
| C-Axis Indexing Precision | Approx. 0.001° |
| Machine Type | Precision Automatic Swiss Lathe |
Documented A20VI specifications identify 18 m/min rapid traverse on X1 and approximately 32 m/min on the other principal rapid axes. (machinetools.com)
CITIZEN A20VI – AXIS TRAVELS / WORK ENVELOPE
| SpecificationDetails | |
|---|---|
| Maximum Machining Diameter | Approx. 20 mm |
| Maximum Machining Length | Approx. 165 mm |
| Maximum Machining Length With Guide Bushing | Approx. 200 mm* |
| Maximum Bar Capacity | Approx. 20 mm |
| Main Spindle Bore | Approx. 20 mm |
| Back Spindle Chucking Diameter | Approx. 20 mm |
| Maximum Guide-Bushingless Length | Approx. 55 mm |
| Workpiece Protrusion From Back Spindle | Approx. 50 mm |
*Some A20-family specifications identify approximately 200 mm machining length with guide bushing; individual 2009 A20VI configurations should be verified. (citizen.de)
CITIZEN A20VI – CAPACITY / WORKHOLDING
| SpecificationDetails | |
|---|---|
| Production Capability | High-Volume Swiss-Type Turning |
| Workholding Configuration | Sliding Headstock / Guide Bushing |
| Maximum Bar Capacity | Approx. 20 mm |
| Maximum Machining Diameter | Approx. 20 mm |
| Sub-Spindle Capacity | Approx. 20 mm |
| Typical Workpiece Size | Small Precision Components |
| Automatic Bar Feeding | Yes |
| Rear-End Machining | Yes |
| Guide Bushing | Configuration Dependent |
CITIZEN A20VI – SPINDLE
| SpecificationDetails | |
|---|---|
| Main Spindle Speed | Approx. 8000 RPM |
| Main Spindle Motor | Approx. 5 HP |
| Main Spindle C-Axis | Full C-Axis |
| C-Axis Indexing | Approx. 0.001° |
| Back Spindle Speed | Approx. 8000 RPM |
| Back Spindle Motor | Approx. 2 HP |
| Back Spindle C-Axis | Full C-Axis |
| Back Spindle Capacity | Approx. 20 mm |
| Spindle Configuration | High-Speed Precision Spindles |
Some A20-family specifications identify a maximum main-spindle speed of 10,000 RPM, while documented 2009 A20VI machines commonly list 8,000 RPM. The exact machine specification should be confirmed before purchase. (machinetools.com)
CITIZEN A20VI – TOOLING / LIVE TOOLING
| SpecificationDetails | |
|---|---|
| Total Tool Positions | Approx. 17–21 |
| Static Turning Tools | Approx. 5 Positions |
| Live Cross Tools | Approx. 4 Positions |
| Front-End Tools | Approx. 4 Positions |
| Back-End Tools | Approx. 4 Positions |
| Live Tool Speed | Approx. 6000 RPM |
| Live Tool Motor | Approx. 1 HP |
| Tooling Type | Static & Rotary Tooling |
| Machining Capability | Turning, Milling, Drilling & Tapping |
Tool-position counts vary between A20VI/A20VIIPL configurations and published specifications, so the exact tooling arrangement should be verified on the individual machine. (cncbul.com)
CITIZEN A20VI – CONTROL SYSTEM
| SpecificationDetails | |
|---|---|
| CNC Control Platform | FANUC / Citizen Cincom Control |
| Programming Capability | G-Code & CNC Programming |
| Main Spindle Control | C-Axis Positioning |
| Sub-Spindle Control | C-Axis Positioning |
| Program Functions | Drilling, Tapping & Milling Cycles |
| Diagnostic Functions | CNC Machine Diagnostics |
| Tool Life Management | Configuration Dependent |
| Rigid Tapping | Available |
| Programming Application | Precision Swiss Machining |
Documented 2009 A20VI machines have been equipped with FANUC controls, while other A20 configurations use Citizen Cincom control platforms. (machinetools.com)
CITIZEN A20VI – COOLANT / DUST / WATER MANAGEMENT
| SpecificationDetails | |
|---|---|
| Coolant Delivery System | Flood / Cutting Coolant |
| Coolant Management | Recirculating System |
| High-Pressure Coolant | Optional / Configuration Dependent |
| Chip Management | Chip Conveyor |
| Mist Collection | Optional / Equipped on Some Machines |
| Parts Removal | Parts Catcher / Conveyor |
| Chip Evacuation | Automated Production System |
| Coolant Pump | Machine-Specific Configuration |
Documented 2009 A20VIIPL machines have been equipped with CoolBlaster high-pressure coolant, chip conveyors, and mist collectors. (machinetools.com)
CITIZEN A20VI – POWER REQUIREMENTS
| SpecificationDetails | |
|---|---|
| Electrical Configuration | Industrial CNC Power |
| Voltage Requirement | Approx. 220V |
| Phase | 3-Phase |
| Main Spindle Motor | Approx. 5 HP |
| Back Spindle Motor | Approx. 2 HP |
| Rotary Tool Motor | Approx. 1 HP |
| Rated Power Consumption | Approx. 7.1 kVA |
| Electrical Installation | Industrial CNC Layout |
Some documented Citizen A20 configurations identify approximately 7.1 kVA rated power consumption, while individual machine electrical requirements should be verified from the machine nameplate. (citizen.co.jp)
CITIZEN A20VI – DIMENSIONS
| SpecificationDetails | |
|---|---|
| Approximate Machine Weight | Approx. 5,000–5,600 lbs |
| Machine Length | Approx. 84–90 in |
| Machine Width | Approx. 47–51 in |
| Machine Height | Approx. 71–88 in |
| Installation Footprint | Compact Production Layout |
| Machine Category | CNC Swiss-Type Automatic Lathe |
Published and used-machine specifications vary depending on bar feeder, chip conveyor, mist collector, and other accessories, with documented machine weights around 5,070–5,620 lbs. (machinetools.com)
CITIZEN A20VI – GENERAL INFORMATION
| SpecificationDetails | |
|---|---|
| Manufacturer | Citizen Machinery |
| Model | A20VI |
| Year | 2009 |
| Machine Category | CNC Swiss-Type Sliding Headstock Lathe |
| Primary Application | Small-Part Precision Machining |
| Maximum Machining Diameter | Approx. 20 mm |
| Maximum Machining Length | Approx. 165 mm |
| Main Spindle Speed | Approx. 8000 RPM |
| Sub-Spindle Speed | Approx. 8000 RPM |
| Common Materials Machined | Steel, Stainless Steel, Brass, Aluminum |
INDUSTRIES THAT USE CITIZEN A20VI
The CITIZEN A20VI is particularly well suited for industries requiring high-volume production of small, precise, and often complex components. Its Swiss-type sliding-headstock architecture provides close support of the workpiece near the cutting tools, making it useful for long, slender, or intricate components that require controlled machining.
Medical manufacturing is one of the major application areas for Swiss-type CNC equipment. The A20VI can be used to produce small medical fittings, surgical components, pins, connectors, bone-related hardware, miniature shafts, and precision instruments. Its live tooling and sub-spindle capability can allow multiple features to be completed within a single automated cycle.
Aerospace manufacturers can utilize the A20VI for producing small precision shafts, bushings, connectors, pins, fittings, fasteners, and instrumentation components. The machine’s C-axis capability allows angular features and cross-machined details to be produced accurately.
Automotive manufacturers can use the machine for small shafts, pins, fuel-system components, sensor hardware, fittings, bushings, and other precision components. The machine’s automated bar-feeding capability makes it particularly suitable for repetitive production runs.
Electronics and telecommunications manufacturers can utilize the A20VI for miniature connectors, contacts, housings, pins, terminals, and precision hardware. These components often require tight dimensional control and consistent repeatability across large production quantities.
Hydraulic and pneumatic equipment manufacturers can use the machine for miniature valves, fittings, sleeves, connectors, stems, and precision fluid-control components. The combination of turning and rear-end machining can reduce the number of separate operations required.
Instrumentation manufacturers can benefit from the A20VI when producing small shafts, threaded components, sensor housings, adjustment screws, connectors, and other precision mechanical components.
General precision machine shops can also use the A20VI for contract production of small components. Its automated bar-fed configuration can allow shops to produce large quantities of identical parts while reducing manual loading and unloading requirements.
The machine is particularly valuable for manufacturers producing components where conventional CNC lathes would require additional fixtures or secondary machining operations. The sliding-headstock design, C-axis capability, live tooling, and sub-spindle can combine several machining processes into one automated production cycle.
High-volume manufacturers can also benefit from the A20VI’s compact footprint. A relatively small floor area can support a machine capable of turning, milling, drilling, tapping, and rear-end machining.
The A20VI is therefore particularly suited to production environments where precision, automation, repeatability, and efficient cycle times are more important than large workpiece capacity.
TYPICAL PARTS CITIZEN A20VI CAN PRODUCE
| Part TypeExamples | |
|---|---|
| Medical Components | Pins, Fittings, Surgical Hardware |
| Aerospace Components | Connectors, Shafts, Precision Fittings |
| Automotive Parts | Pins, Bushings, Sensor Components |
| Electronics Hardware | Contacts, Terminals, Connectors |
| Hydraulic Components | Valves, Fittings, Sleeves |
| Instrumentation Parts | Shafts, Housings, Adjustment Components |
| Precision Hardware | Screws, Pins, Small Bushings |
| Industrial Components | Couplings, Stems, Miniature Fittings |
WHY CHOOSE CITIZEN A20VI
The CITIZEN A20VI is designed for manufacturers seeking precision small-part machining capability combined with automated Swiss-type production. Its approximately 20 mm maximum machining diameter makes it particularly appropriate for components that require high dimensional consistency and repeatable production.
One of the machine’s biggest advantages is its sliding-headstock architecture. The workpiece is supported close to the cutting tools, reducing the unsupported length of slender material during machining. This can be particularly beneficial when producing long, narrow components that might experience deflection on conventional fixed-headstock turning centers.
The machine’s live tooling further increases its versatility. Documented configurations provide multiple rotary-tool positions capable of approximately 6,000 RPM. These tools can perform cross drilling, milling, tapping, and other secondary operations without removing the component from the primary machining setup. (toolquipusa.com)
The sub-spindle provides another significant production advantage. After primary machining, the workpiece can be transferred to the back spindle for rear-end operations. This allows front and back features to be produced within the same automated production cycle.
Full C-axis capability on the main and sub-spindles provides accurate angular positioning for milling and drilling operations. Published specifications identify approximately 0.001-degree C-axis indexing, supporting precise cross-machined features. (machinetools.com)
The machine’s high spindle speed is also important for small-diameter machining. With documented 2009 configurations operating at approximately 8,000 RPM, the spindle can provide suitable cutting speeds for many small-diameter materials and precision components.
Another advantage is automatic bar feeding. When paired with an appropriate magazine bar feeder, the A20VI can continuously process raw material with limited operator intervention. Documented 2009 machines have been equipped with Edge Technologies C-320 12-foot magazine bar feeders. (machinetools.com)
The machine’s compact footprint is another benefit for production facilities. Manufacturers can add automated small-part machining capacity without requiring the floor space associated with larger conventional CNC turning centers.
The A20VI also supports multiple machining operations within one machine. Turning, drilling, tapping, milling, front-end work, and back-end machining can all be incorporated into the production process depending on the machine’s tooling configuration.
Chip management and coolant systems are also important when running high-volume Swiss machining. Many used A20VI machines include chip conveyors, coolant systems, parts catchers, and mist collection equipment, helping support continuous production.
For manufacturers producing large quantities of small, complex, precision components, the A20VI provides a practical combination of automation, machining flexibility, and compact machine design.
The machine is particularly useful when reducing secondary operations is important. Completing multiple features within one automated cycle can reduce handling, improve repeatability, and simplify production flow.
For manufacturers seeking a proven CNC Swiss-type machine for small-diameter production, the CITIZEN A20VI remains a capable platform for precision machining applications.
WHY BUY USED CITIZEN A20VI
Purchasing a used 2009 CITIZEN A20VI allows manufacturers to obtain established Swiss-type CNC machining capability at a substantially lower acquisition cost than purchasing a new precision automatic lathe. For manufacturers already producing small-diameter components, a used A20VI can provide an economical way to expand production capacity.
The machine’s 20 mm machining capacity makes it particularly useful for high-volume production of small components. A properly maintained A20VI can continue producing precision parts for many years when its guideways, spindle, ballscrews, tooling systems, control, coolant equipment, and bar-feeding equipment are properly maintained.
One of the biggest advantages of purchasing used Swiss machinery is access to automation. Many used A20VI machines are sold with bar feeders and chip-management equipment already installed. This can reduce the additional investment required to establish an automated production cell.
Documented 2009 A20VI machines have been offered with Edge Technologies C-320 magazine bar feeders, chip conveyors, parts catchers, coolant systems, and mist collectors. (machinetools.com)
The live tooling and sub-spindle also provide significant production flexibility. A manufacturer can potentially perform turning, cross milling, drilling, tapping, and rear-end operations without transferring the component between separate machines.
This can be particularly valuable for small components where manual handling can represent a substantial percentage of total production time. Automated transfer between the main and sub-spindle can help reduce operator involvement.
Another advantage of used equipment is availability. If a suitable A20VI is already available with the required bar feeder, tooling, and accessories, manufacturers can potentially bring additional machining capacity online faster than purchasing and waiting for a new machine.
Before purchasing a used A20VI, buyers should carefully inspect the main spindle, sub-spindle, guide bushing, sliding headstock, axis movement, live-tool spindles, C-axis positioning, tooling stations, bar feeder, chip conveyor, coolant system, and CNC control.
The guide-bushing system deserves particular attention because it is fundamental to Swiss-type machining. Buyers should inspect the guide bushing, guide-bushing holder, alignment, and related components for wear.
The bar feeder should also be tested thoroughly. Magazine alignment, material loading, remnant handling, bar-pusher operation, and communication between the feeder and CNC control should all be verified before purchase.
Spindle condition is another important consideration. Buyers should check spindle noise, vibration, temperature, runout, indexing performance, and overall machining quality.
The live tooling system should also be tested because rotary tools are important to the machine’s multi-operation capability. Buyers should verify live-tool speed, rotation, indexing, and tooling-holder condition.
Machine history and maintenance records can provide additional insight into the equipment’s previous operating environment. Machines that have been properly serviced and maintained may require less preparation before being returned to production.
For manufacturers seeking automated small-part production capability without the capital expense of new Swiss machinery, a used CITIZEN A20VI can provide a practical production solution.
Its combination of sliding-headstock machining, live tooling, C-axis capability, sub-spindle, and automated bar feeding makes it particularly valuable for manufacturers producing precision components in repetitive quantities.
HOW MUCH DOES A USED CITIZEN A20VI COST?
The price of a used 2009 CITIZEN A20VI depends on machine condition, spindle hours, cutting hours, control configuration, bar feeder, tooling package, sub-spindle condition, guide-bushing equipment, chip conveyor, coolant system, maintenance history, and overall market demand.
Current and recent used-machine listings show significant variation depending on configuration and condition. One 2009 CITIZEN A20VI listing has been advertised at approximately $77,000, while other 2009 A20VI/A20VIIPL machines are offered on a request-for-quote basis. These asking prices should not be treated as confirmed transaction values. (machinetools.com)
A practical used-market range for a 2009 CITIZEN A20VI can be approximately $35,000 to $80,000+, depending heavily on condition, automation equipment, tooling, operating hours, and included accessories. Machines equipped with high-quality magazine bar feeders, live tooling, sub-spindles, chip conveyors, high-pressure coolant, and complete tooling packages can command substantially higher asking prices than basic configurations.
Machine condition is one of the most important pricing factors. Buyers should inspect the sliding headstock, guide bushing, main spindle, sub-spindle, live-tool spindles, C-axis positioning, axis movement, lubrication system, coolant system, and CNC control.
Spindle hours and cutting hours should be reviewed whenever available. Two machines of the same model and year can have substantially different market values depending on their production history.
The bar feeder can also have a major effect on total value. A properly functioning long magazine bar feeder can transform the machine into a highly automated production cell, while a machine with a damaged or missing feeder may require additional investment before high-volume production can begin.
The tooling package should also be considered. Swiss-type machines can require specialized guide bushings, holders, collets, live-tool holders, sleeves, and other accessories. A machine sold with a comprehensive tooling package may provide greater immediate production value.
Chip management and coolant systems can also affect pricing. Documented A20VI machines have been equipped with chip conveyors, coolant systems, high-pressure coolant, mist collectors, and parts conveyors. (machinetools.com)
The CNC control is another important consideration. FANUC-based controls are documented on several 2009 A20VI machines, while Citizen Cincom control configurations are also found across the A20 platform. Buyers should verify the exact control and ensure that it is operating correctly.
Transportation and installation costs should also be included in the overall acquisition budget. Although the A20VI is compact compared with larger CNC turning centers, a complete machine with magazine bar feeder, chip conveyor, coolant equipment, and accessories can require specialized transportation and installation.
Electrical requirements should be verified before delivery. Documented Citizen A20 specifications identify approximately 7.1 kVA rated power consumption, while actual requirements depend on the machine’s exact configuration and accessories. (citizen.co.jp)
Buyers should also budget for tooling, guide bushings, collets, coolant, machine inspection, leveling, and any repairs identified during commissioning.
The age of the machine makes actual condition particularly important. A well-maintained 2009 A20VI with a strong service history, functional bar feeder, good spindle condition, and complete tooling package can provide substantially different value from a machine that has been heavily used or poorly maintained.
For manufacturers requiring automated precision machining of components up to approximately 20 mm in diameter, the used 2009 CITIZEN A20VI provides a combination of Swiss-type workholding, live tooling, C-axis machining, sub-spindle capability, and automated production flexibility.
Its approximately 20 mm bar capacity, 8,000 RPM-class spindle configuration, approximately 165 mm machining length, live-tool capability, full C-axis positioning, and sub-spindle make it particularly suitable for high-volume small-part manufacturing.
For machine shops seeking to expand precision Swiss machining capacity while controlling equipment acquisition costs, the used CITIZEN A20VI remains a practical CNC production platform for small, complex, and repeatable components.
Related Products
-
CITIZEN - A20VII
VIEW MACHINE -
CITIZEN - L20VIII
VIEW MACHINE -
CITIZEN - L20VIII
VIEW MACHINE -
CITIZEN - A20VII
VIEW MACHINE