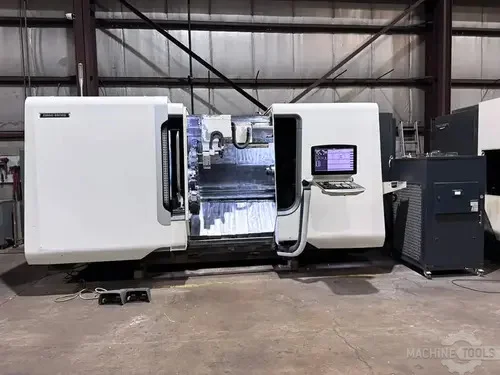
DMG MORI CTX BETA 1250 4A – 2016
USED DMG MORI CTX BETA 1250 4A – 2016
The 2016 DMG MORI CTX beta 1250 4A is a high-productivity CNC production turning center designed for manufacturers requiring advanced 4-axis machining, parallel turning operations, Y-axis capability, and efficient complete machining of medium-to-large cylindrical components. Manufactured by DMG MORI, the CTX beta 1250 4A incorporates the company’s TWIN concept, using two tool carriers to perform multiple machining operations simultaneously. This configuration allows manufacturers to reduce cycle times, improve spindle utilization, and increase production output compared with conventional single-turret turning centers. DMG MORI specifies the CTX beta 1250 4A with a maximum workpiece diameter of approximately 13.4 inches, maximum workpiece length of approximately 44.7 inches, and maximum bar capacity of approximately 4 inches.
The CTX beta 1250 4A utilizes a rigid production-oriented machine structure engineered to provide stability during demanding turning operations while maintaining accuracy during continuous production. The machine incorporates two turrets and two Y-axis systems, allowing tools to approach the workpiece from multiple positions and supporting efficient machining of complex bar, shaft, and chuck components. The TWIN concept allows both tool carriers to participate in production operations, making the machine particularly suitable for manufacturers producing repeated components in medium- and high-volume environments.
The main and counter spindles are designed for coordinated production machining, with the CTX beta 1250 4A platform offering spindle speeds of approximately 5,000 RPM and substantial spindle torque for heavy-duty turning applications. The machine can be equipped with two 12-station VDI 40 turrets with driven tooling, while DirectDrive turret configurations can provide significantly higher driven-tool speeds. This combination allows turning, drilling, tapping, milling, and other secondary operations to be completed without transferring the workpiece to another machine.
The 2016 CTX beta 1250 4A is capable of machining aluminum, carbon steel, stainless steel, alloy steel, cast iron, brass, titanium, and other engineering materials commonly used in industrial production. Typical applications include shafts, flanges, valve bodies, hydraulic components, couplings, sleeves, bearing housings, automotive components, heavy-equipment parts, and precision industrial hardware requiring multiple machining operations.
One of the machine’s biggest advantages is its ability to perform parallel machining with two tool carriers. While one turret performs a turning operation, the second turret can perform another machining operation, reducing idle time and improving overall production efficiency. The counter spindle also allows components to be transferred for additional machining operations without manual repositioning.
The machine’s Y-axis capability further expands its machining flexibility by allowing off-center drilling, milling, and other driven-tool operations. Depending on the exact configuration, each turret can have Y-axis movement, making the CTX beta 1250 4A particularly useful for complex shaft and chuck components requiring secondary machining features.
Many CTX beta 1250 4A machines can also be integrated with bar feeders, chip conveyors, parts handling equipment, automation systems, probing, and other production accessories. DMG MORI designed the platform with automation and serial production in mind, allowing manufacturers to develop highly efficient unattended or semi-unattended production processes.
Industries including automotive manufacturing, aerospace, energy, oil and gas, hydraulic equipment, heavy machinery, transportation, industrial automation, and general precision machining can benefit from the machine’s combination of production turning capacity, twin-turret operation, Y-axis machining, and counter-spindle functionality.
Because of its strong production capability, parallel machining architecture, substantial work envelope, and flexible tooling configuration, the 2016 DMG MORI CTX beta 1250 4A remains a capable CNC production turning center for manufacturers seeking increased machining productivity.
DMG MORI CTX BETA 1250 4A – AXIS
| SpecificationDetails | |
|---|---|
| Machine Configuration | CNC Production Turning Center |
| Axis Configuration | X1, Y1, Z1, X2, Y2, Z2 |
| X-Axis Travel | Approx. 11.8 in / 300 mm |
| Y-Axis Travel | Approx. ±2.4 in / ±60 mm |
| Z-Axis Travel | Approx. 46.1 in / 1,170 mm |
| Turret Configuration | Twin Turret |
| Number of Machining Axes | 4-Axis Production Capability |
| Parallel Machining | Yes |
The CTX beta 1250 4A uses DMG MORI’s TWIN concept with two tool carriers, allowing parallel machining operations and improved utilization of the machining envelope.
DMG MORI CTX BETA 1250 4A – AXIS TRAVELS / WORK ENVELOPE
| SpecificationDetails | |
|---|---|
| Maximum Workpiece Diameter | Approx. 13.4 in / 340 mm |
| Maximum Workpiece Length | Approx. 44.7 in / 1,135 mm |
| Maximum Bar Capacity | Approx. 4 in / 102 mm |
| Maximum X-Axis Travel | Approx. 11.8 in |
| Maximum Y-Axis Travel | Approx. 4.7 in |
| Maximum Z-Axis Travel | Approx. 46.1 in |
| Maximum Turning Diameter | Approx. 13.4 in |
| Turning Length | Up to Approx. 47.2 in Depending on Configuration |
DMG MORI’s published specifications for the CTX beta 1250 4A list a maximum workpiece diameter of approximately 13.4 inches, maximum workpiece length of approximately 44.7 inches, and maximum bar diameter of approximately 4 inches.
DMG MORI CTX BETA 1250 4A – CAPACITY / WORKHOLDING
| SpecificationDetails | |
|---|---|
| Machine Type | CNC Twin-Turret Turning Center |
| Production Capability | 4-Axis Complete Machining |
| Maximum Workpiece Diameter | Approx. 340 mm |
| Maximum Workpiece Length | Approx. 1,135 mm |
| Bar Work Capability | Up to Approx. 102 mm |
| Workholding Compatibility | Chuck, Bar & Shaft Work |
| Counter Spindle | Standard |
| Automation Ready | Yes |
| Production Environment | Medium & High-Volume Manufacturing |
The CTX beta 1250 4A was designed around two turrets and a counter spindle, making it suitable for complete machining of bars, shafts, and chuck components.
DMG MORI CTX BETA 1250 4A – SPINDLE
| SpecificationDetails | |
|---|---|
| Main Spindle Type | Integrated Motor Spindle |
| Main Spindle Speed | Approx. 5,000 RPM |
| Counter Spindle Speed | Approx. 5,000 RPM |
| Main Spindle Power | Approx. 64 HP |
| Main Spindle Torque | Approx. 265 ft-lb |
| Counter Spindle | Integrated Motor Spindle |
| Spindle Bore / Clamping Tube | Approx. 2.6 in |
| C-Axis Capability | Yes |
| Spindle Application | Heavy-Duty Production Turning |
DMG MORI lists the CTX beta 1250 4A with main and counter spindles capable of approximately 5,000 RPM, with the published 4A specification showing approximately 42.9 kW and 265.5 ft-lb for the main spindle configuration.
DMG MORI CTX BETA 1250 4A – TOOL CHANGER / TURRETS
| SpecificationDetails | |
|---|---|
| Turret Configuration | Two Turrets |
| Standard Turret Capacity | 12 Stations Each |
| Turret Interface | VDI 40 |
| Driven Tooling | Yes |
| Driven Tool Speed | Approx. 4,000 RPM |
| Optional DirectDrive Turret | Available |
| DirectDrive Turret Speed | Up to Approx. 10,000 RPM |
| Tooling Capability | Turning, Drilling, Milling & Tapping |
| Parallel Tool Operation | Yes |
The standard CTX beta 1250 4A configuration uses two 12-fold VDI 40 turrets with driven tooling, while an optional DirectDrive turret can provide up to approximately 10,000 RPM.
DMG MORI CTX BETA 1250 4A – CONTROL SYSTEM
| SpecificationDetails | |
|---|---|
| CNC Control Platform | Siemens CNC Configuration |
| Programming Capability | G-Code & Workshop-Oriented Programming |
| Control Interface | DMG MORI / Siemens |
| ShopTurn Capability | Available |
| DIN / ISO Programming | Yes |
| Technology Cycles | DMG MORI Technology Cycles |
| Operator Interface | ERGOline Control Panel |
| Production Data Management | Configuration Dependent |
The CTX beta 1250 platform was offered with Siemens control technology and workshop-oriented ShopTurn programming, providing operators with both conversational and DIN/ISO programming capabilities.
DMG MORI CTX BETA 1250 4A – COOLANT / DUST / WATER MANAGEMENT
| SpecificationDetails | |
|---|---|
| Coolant Delivery System | Flood Coolant |
| Coolant Management | Integrated CNC Coolant System |
| Chip Management | Chip Conveyor / Chip Collection |
| High-Pressure Coolant | Optional / Configuration Dependent |
| Coolant Filtration | Configuration Dependent |
| Spindle Cooling | Water-Cooled Spindle Motors |
| Chip Evacuation | Enclosed Machining Area |
| Production Cooling | Continuous Industrial Coolant System |
The CTX beta 1250 platform incorporates thermal-management features including water-cooled spindle motors, supporting consistent performance during extended production cycles.
DMG MORI CTX BETA 1250 4A – POWER REQUIREMENTS
| SpecificationDetails | |
|---|---|
| Electrical Configuration | Industrial CNC Power System |
| Power Requirement | Configuration Dependent |
| Main Spindle Power | Approx. 64 HP |
| Turret Drive Power | Configuration Dependent |
| Voltage | Region / Machine Configuration Dependent |
| Phase | 3-Phase Industrial Power |
| Pneumatic Requirement | Standard Shop Air |
| Installation | Industrial CNC Environment |
Actual electrical requirements can vary according to the 2016 machine’s spindle configuration, coolant system, chip conveyor, automation equipment, transformer, and other installed options. Buyers should verify the machine’s electrical documentation before installation.
DMG MORI CTX BETA 1250 4A – DIMENSIONS
| SpecificationDetails | |
|---|---|
| Approximate Machine Weight | Configuration Dependent |
| Machine Length | Configuration Dependent |
| Machine Width | Configuration Dependent |
| Machine Height | Configuration Dependent |
| Installation Footprint | Large Production Layout |
| Chip Conveyor Space | Additional Space Required |
| Bar Feeder Space | Additional Space Required When Equipped |
| Automation Space | Additional Space Required When Equipped |
Machine dimensions and total weight can vary according to the installed chip conveyor, bar feeder, automation equipment, coolant system, tooling configuration, and other factory-installed options. Buyers should obtain the original machine layout before transportation and installation.
DMG MORI CTX BETA 1250 4A – GENERAL INFORMATION
| SpecificationDetails | |
|---|---|
| Manufacturer | DMG MORI |
| Model | CTX beta 1250 4A |
| Year | 2016 |
| Machine Category | CNC Production Turning Center |
| Machine Configuration | Twin-Turret 4-Axis Turning |
| Primary Application | Complete Production Machining |
| Spindle Configuration | Main Spindle & Counter Spindle |
| Turret Configuration | Two Driven-Tool Turrets |
| Common Materials Machined | Steel, Aluminum, Stainless Steel, Brass |
The CTX beta 1250 4A belongs to the production-oriented CTX beta family and was developed around a twin-tool-carrier concept for efficient parallel machining.
INDUSTRIES THAT USE DMG MORI CTX BETA 1250 4A
The DMG MORI CTX beta 1250 4A is well suited for industries requiring high-volume production of cylindrical, shaft-type, and complex turned components. Automotive manufacturers can use the machine for producing shafts, hubs, transmission components, bearing housings, sleeves, couplings, and other drivetrain components requiring multiple machining operations.
Aerospace manufacturers can utilize the CTX beta 1250 4A for machining precision shafts, adapters, flanges, housings, fittings, and structural components manufactured from aluminum, stainless steel, titanium, and specialty alloys. The machine’s twin-turret configuration allows multiple tools to participate in the production process while maintaining consistent workholding.
Oil and gas manufacturers can use the machine for producing valve components, sleeves, couplings, hydraulic components, fittings, flanges, and other cylindrical hardware. The combination of substantial bar capacity and high spindle torque makes the machine suitable for a broad range of industrial components.
Hydraulic and pneumatic component manufacturers can use the CTX beta 1250 4A for machining cylinders, valve bodies, manifolds, shafts, pistons, connectors, and precision sleeves. Y-axis capability allows additional off-center machining operations without requiring a separate machining center.
Heavy equipment manufacturers frequently require large quantities of shafts, pins, bushings, housings, couplings, and support components. The CTX beta 1250 4A can support these applications through its long turning capacity and parallel machining architecture.
Industrial automation manufacturers can also utilize the machine for machining actuator shafts, robotic components, drive components, precision housings, and custom production hardware.
General contract machine shops can benefit from the machine’s ability to perform multiple operations in a single production cycle. The two-turret configuration allows shops to reduce non-cutting time and improve machine utilization when producing repeat components.
The machine is particularly useful for manufacturers seeking production-oriented CNC turning equipment capable of combining turning, driven-tool machining, Y-axis operations, and counter-spindle machining within one integrated platform.
TYPICAL PARTS DMG MORI CTX BETA 1250 4A CAN PRODUCE
| Part TypeExamples | |
|---|---|
| Automotive Components | Shafts, Hubs, Bearing Housings |
| Aerospace Components | Adapters, Flanges, Precision Shafts |
| Oil & Gas Hardware | Valves, Fittings, Couplings |
| Hydraulic Components | Cylinders, Pistons, Manifolds |
| Industrial Components | Bushings, Sleeves, Housings |
| Heavy Equipment Parts | Pins, Shafts, Support Components |
| Precision Hardware | Threaded Parts, Connectors, Flanges |
WHY CHOOSE DMG MORI CTX BETA 1250 4A
The DMG MORI CTX beta 1250 4A is designed for manufacturers seeking high-productivity CNC turning capability with two tool carriers, Y-axis machining, a counter spindle, and driven tooling. Its TWIN concept allows two turrets to perform machining operations in parallel, helping reduce idle time and improve overall production efficiency.
One of the machine’s biggest advantages is its ability to process components using two tool carriers rather than relying on a single turret. This architecture can reduce cycle times because different machining operations can be coordinated within the same production cycle. For repetitive production work, improved tool utilization and reduced non-cutting time can contribute significantly to overall manufacturing efficiency.
The counter spindle provides another important production advantage. Components can be transferred between the main and counter spindles for additional machining operations without requiring manual removal and repositioning. This supports complete machining of shafts, bars, and chuck components while improving consistency between machining operations.
Y-axis capability expands the machine’s ability to perform off-center drilling, milling, tapping, and other driven-tool operations. This can reduce the need to transfer components to a separate machining center for secondary features.
The two VDI 40 turrets provide substantial tooling flexibility, with 12 stations per turret in the standard configuration. Driven tools allow the machine to perform additional machining operations beyond conventional turning. Optional DirectDrive turret technology can provide significantly higher driven-tool speeds for demanding applications.
The machine’s main and counter spindles also provide substantial turning performance. DMG MORI specifies approximately 5,000 RPM spindle speed and substantial torque for the CTX beta 1250 4A, making it suitable for both production turning and heavier material-removal applications.
Thermal stability is another important consideration. Water-cooled spindle motors and measurement technologies were incorporated into the CTX beta platform to support consistent machining performance during extended operating periods.
Automation compatibility further increases the machine’s production potential. Bar feeders, chip conveyors, workpiece handling equipment, and other automation systems can be integrated into production cells to reduce manual intervention.
For manufacturers seeking a production-oriented CNC turning center capable of combining twin-turret machining, Y-axis capability, driven tooling, and counter-spindle operations, the CTX beta 1250 4A provides a versatile and highly productive manufacturing platform.
WHY BUY USED DMG MORI CTX BETA 1250 4A
Purchasing a used 2016 DMG MORI CTX beta 1250 4A allows manufacturers to acquire a sophisticated twin-turret CNC production turning center while reducing the capital investment required compared with purchasing a new high-productivity production machine. The CTX beta 1250 4A combines multiple machining capabilities within one platform, allowing manufacturers to expand production without necessarily adding several separate machines.
A major advantage of purchasing used equipment is the availability of proven production technology at a lower acquisition cost. A properly maintained CTX beta 1250 4A can continue providing twin-turret machining, driven tooling, Y-axis capability, counter-spindle operations, and substantial turning capacity many years after its original installation.
The machine is particularly attractive for manufacturers producing repeat components because the twin-turret TWIN concept allows multiple operations to be performed simultaneously. This can help reduce cycle time and increase spindle utilization compared with traditional single-turret production turning equipment.
Another advantage is the machine’s broad material capability. Manufacturers can use the CTX beta 1250 4A for aluminum, steel, stainless steel, brass, cast iron, and other industrial materials. This makes it suitable for diverse production environments where multiple types of components need to be manufactured.
Many used machines are also sold with production accessories already installed. Depending on the individual machine, buyers may find bar feeders, chip conveyors, driven tooling, probing systems, tooling packages, coolant equipment, parts handling systems, and other accessories included with the purchase.
Before purchasing a used CTX beta 1250 4A, buyers should carefully inspect the main spindle, counter spindle, turret indexing, driven-tool operation, Y-axis accuracy, guideways, ball screws, lubrication system, coolant system, chip conveyor, hydraulic system, and CNC control.
Spindle hours and maintenance history are particularly important when evaluating an older production turning center. Buyers should request machine-hour information, service records, recent inspection reports, and evidence of regular preventive maintenance whenever available.
The machine’s exact configuration should also be verified because optional features can significantly change its production capability and market value. A machine equipped with DirectDrive turrets, advanced tooling, automation, bar feeding, and additional production accessories can have substantially greater value than a basic configuration.
For manufacturers seeking a dependable production turning platform with twin-turret machining, Y-axis capability, counter-spindle operation, and driven tooling, a properly maintained used 2016 DMG MORI CTX beta 1250 4A can provide substantial manufacturing capability at a reduced equipment acquisition cost.
HOW MUCH DOES A USED DMG MORI CTX BETA 1250 4A COST?
The price of a used 2016 DMG MORI CTX beta 1250 4A depends on several factors including machine condition, spindle hours, control configuration, tooling, turret condition, installed automation, bar feeder, chip conveyor, maintenance history, and geographic location. Production turning machines can have significant differences in used-market value depending on their configuration and remaining production capability.
A practical used-market estimate for a 2016 DMG MORI CTX beta 1250 4A is approximately $90,000 to $180,000, although exceptionally well-equipped, low-hour machines can potentially command prices outside this range. Machines with higher operating hours, limited accessories, or significant maintenance requirements may be priced toward the lower end.
Machine configuration has a major influence on pricing. A CTX beta 1250 4A equipped with two driven-tool turrets, DirectDrive technology, extensive tooling, probing, bar feeding, chip management, and automation can command a substantially higher price than a machine with basic equipment.
The spindle and turret condition should be carefully evaluated before determining the actual market value. Buyers should inspect spindle bearings, spindle runout, C-axis positioning, turret indexing, driven-tool performance, Y-axis movement, guideway condition, ball screws, lubrication, hydraulics, and coolant systems.
The condition of the CNC control is also important. A machine with a properly functioning Siemens control, documented maintenance history, clean electrical cabinet, and reliable machine operation generally offers a different ownership proposition than equipment requiring major electrical or control-system repairs.
Accessories can also influence the final purchase price. A bar feeder, chip conveyor, parts catcher, probing system, tooling package, high-pressure coolant, and automation equipment can significantly improve the machine’s production value.
Transportation, rigging, installation, electrical preparation, tooling, coolant, and commissioning costs should also be included when calculating the total acquisition budget. These expenses can vary considerably depending on the machine’s location and final installation site.
The CTX beta 1250 4A remains a production-focused CNC turning platform with substantial machining capacity, twin-turret operation, Y-axis capability, driven tooling, and counter-spindle functionality. For manufacturers seeking to expand production capability while controlling the initial equipment investment, a properly maintained used 2016 DMG MORI CTX beta 1250 4A can provide a strong combination of machining flexibility and production capacity.
Related Products
-

MORI SEIKI - NH4000DCG
VIEW MACHINE -

MORI SEIKI - NMV5000DCG
VIEW MACHINE -
MORI SEIKI - DURAVERTICAL 5100
VIEW MACHINE -
ON SALE

MORI SEIKI - NL2500
VIEW MACHINE